


A drive-in storage facility, also known as a drive-in racking system, is a high-density storage solution that allows forklifts to drive directly into the storage lanes to access pallets. As a drive supplier, I've seen firsthand how this type of storage facility can bring numerous benefits to businesses of all sizes. In this blog post, I'll explore the key advantages of a drive-in storage facility and why it might be the right choice for your storage needs.
High Storage Density
One of the most significant benefits of a drive-in storage facility is its ability to maximize storage space. Traditional pallet racking systems, such as selective racking, require aisles between each row of pallets, which can take up a significant amount of floor space. In contrast, drive-in storage systems eliminate the need for multiple aisles, allowing for more pallets to be stored in a given area.
Drive-in racks are designed with a single entry and exit point, and pallets are stored in a last-in, first-out (LIFO) configuration. This means that forklifts can drive directly into the racking structure to place or retrieve pallets, making efficient use of the available vertical and horizontal space. As a result, drive-in storage facilities can typically store up to 75% more pallets than selective racking systems, making them an ideal solution for businesses with limited warehouse space.
Cost-Effective
Another advantage of a drive-in storage facility is its cost-effectiveness. By maximizing storage density, drive-in racks can help businesses reduce their overall warehouse footprint, which can lead to significant cost savings in terms of rent, utilities, and maintenance. Additionally, because drive-in racks require fewer structural components than traditional racking systems, they can be less expensive to install and maintain.
In addition to the initial cost savings, drive-in storage facilities can also help businesses save money in the long run by reducing the need for additional storage space. As businesses grow and their inventory needs increase, they may need to expand their warehouse facilities to accommodate the additional stock. By using a drive-in storage system, businesses can make the most of their existing warehouse space, delaying or eliminating the need for costly warehouse expansions.
Improved Inventory Management
Drive-in storage facilities can also improve inventory management by providing easy access to pallets and reducing the risk of product damage. Because forklifts can drive directly into the racking structure to place or retrieve pallets, there is less need for manual handling, which can reduce the risk of accidents and product damage. Additionally, because pallets are stored in a LIFO configuration, it is easier to manage inventory turnover and ensure that older stock is used first.
Drive-in storage facilities can also be equipped with a variety of inventory management tools, such as barcode scanners and inventory tracking software, to help businesses keep track of their inventory levels and location. This can help businesses improve their order fulfillment processes, reduce the risk of stockouts, and improve overall customer satisfaction.
Flexibility
Drive-in storage facilities are also highly flexible and can be customized to meet the specific needs of different businesses. Drive-in racks can be designed to accommodate a variety of pallet sizes and weights, and they can be configured to fit into different warehouse layouts and spaces. Additionally, drive-in racks can be easily modified or expanded as a business's inventory needs change, making them a versatile storage solution for businesses of all sizes.
For example, businesses that need to store a large volume of the same product can use a drive-in storage system to maximize storage density and improve inventory management. On the other hand, businesses that need to store a variety of different products can use a drive-in storage system in combination with other types of racking systems, such as selective racking or push-back racking, to create a customized storage solution that meets their specific needs.

Safety
Safety is always a top priority in any warehouse environment, and drive-in storage facilities are no exception. Drive-in racks are designed with a variety of safety features, such as guide rails, anti-collapse nets, and load backrests, to help prevent accidents and protect workers and inventory. Additionally, because drive-in racks are designed with a single entry and exit point, it is easier to control traffic flow and reduce the risk of collisions between forklifts.
In addition to the safety features built into the drive-in racking system, businesses can also implement a variety of safety protocols and training programs to ensure that their workers are properly trained and equipped to operate forklifts safely in a drive-in storage facility. This can help reduce the risk of accidents and injuries, and it can also help businesses comply with OSHA regulations and other safety standards.
Our Drive Products for Storage Facilities
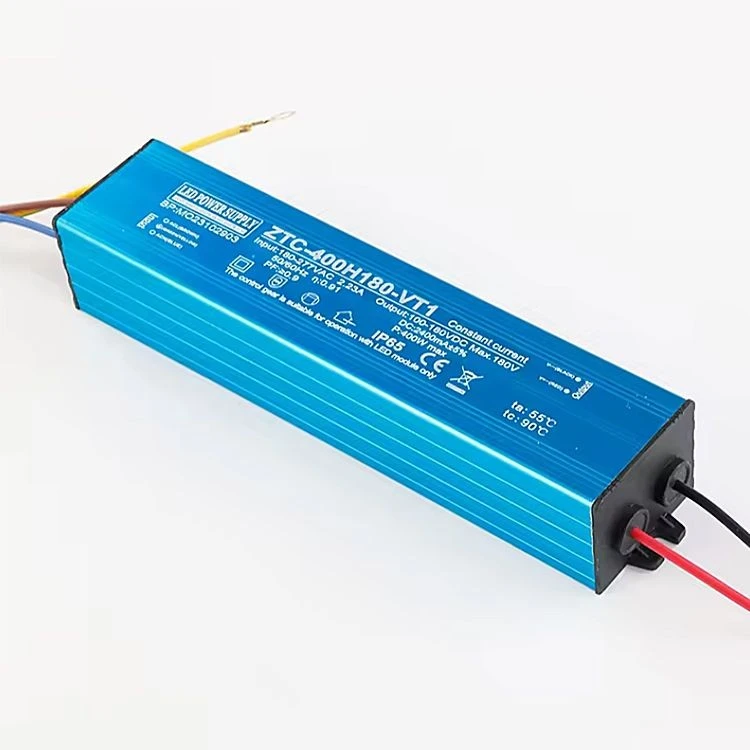
As a drive supplier, we offer a range of high-quality drive products that are suitable for use in drive-in storage facilities. Our drives are designed to provide reliable and efficient power to forklifts and other material handling equipment, helping to ensure smooth and safe operation in the warehouse environment.
One of our popular products is the AC12V 60W Square Waterproof Transformer. This transformer is designed to provide a stable and reliable power supply to forklift lights and other electrical components, even in wet or harsh environments. It features a waterproof design and a high-efficiency transformer core, making it a durable and energy-efficient choice for drive-in storage facilities.
Another product we offer is the AC12V 105W Square Waterproof Transformer. This transformer is similar to the AC12V 60W model, but it provides a higher power output, making it suitable for use with larger forklift lights and other electrical components. It also features a waterproof design and a high-efficiency transformer core, ensuring reliable and efficient operation in the warehouse environment.
We also offer the AC110V-220V To DC65-80V 50W Drive, which is designed to convert AC power to DC power for use with a variety of electrical components in forklifts and other material handling equipment. This drive features a high-efficiency design and a wide input voltage range, making it a versatile and reliable choice for drive-in storage facilities.
Contact Us for Your Storage Needs
If you're interested in learning more about the benefits of a drive-in storage facility or if you're looking for high-quality drive products for your warehouse, we'd love to hear from you. Our team of experts can help you determine the best storage solution for your business needs and provide you with the products and support you need to ensure the success of your storage operation.
Whether you're a small business looking to maximize your warehouse space or a large corporation looking to improve your inventory management, a drive-in storage facility and our drive products can help you achieve your goals. Contact us today to start the conversation and take the first step towards a more efficient and cost-effective storage solution.
References
- "Drive-In and Drive-Through Racking Systems," Warehouse Rack & Shelving.
- "Benefits of Drive-In Racking," Steel King Industries.
- "Maximizing Warehouse Space with Drive-In Racking," Crown Equipment Corporation.